Equipment, Offload & Stackers
Material Handling & Stackers
The offload side of the line. Runout, kickers, lift tables, bundlers, and exit conveyors that match the speed of the mill.
A line is only as fast as the offload behind it. Parts exit the cutoff every few seconds. Someone, or something, has to get them off the runout and into a bundle before the next batch arrives. We engineer that side of the system as carefully as the forming side.
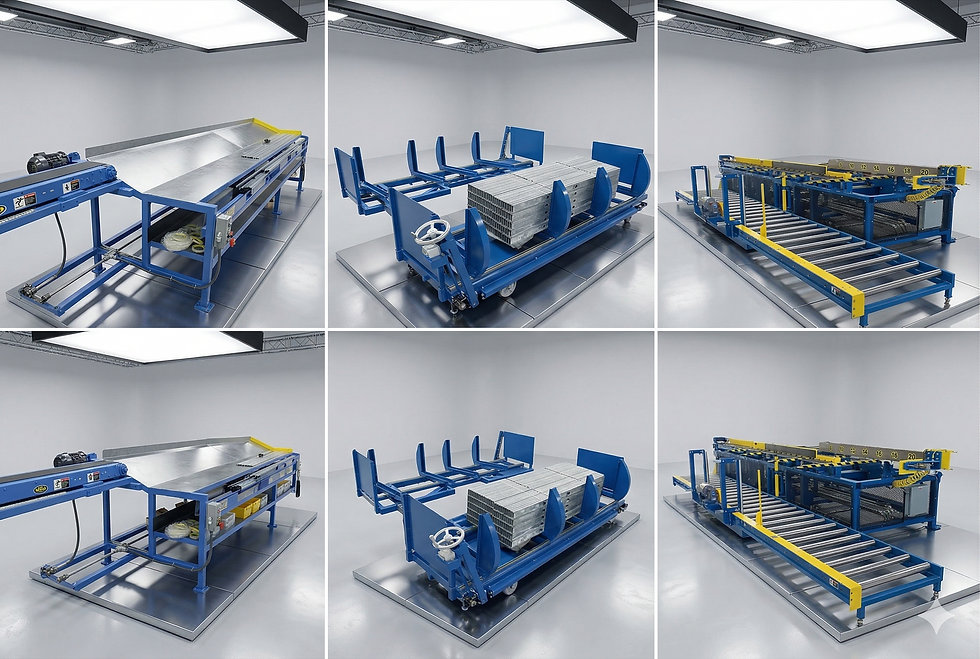
TEKFAB offload systems scale from a simple non powered runout with manual stacking up to a fully automated kicker-lift-bundler-strap-exit chain that runs without an operator between coil change and full-pallet ready. The right scope depends on bundle weight, plant footprint, labor model, and how often the line changes section.

Where this fits
Lines that pair with serious offload.
Inside the offload
Kickers, lifts, indexers, and bundlers built to match the line.
Kicker length is sized to the part. A 12 ft kicker is enough for a 10 ft profile. A 36 ft kicker is what a 30 ft profile. Lift tables drop in 1/2-inch increments under servo control so a 9,500 lb HG bundle lands flat. Indexers nest light gauge accessories two-up or four-up before they reach the strap.
Auto-bundlers and strap stations close the loop. The operator sets the bundle count at the HMI and the line drops a strapped, square, count-correct bundle onto the exit conveyor. The forklift driver does not have to count parts.

Capability envelope
Add a Title
Add a Title

Three stages of automation
From runout plus operator to lights out bundle.
Stage 1 keeps the operator in the loop. Stage 2 takes over the lift. Stage 3 takes the full control. Most customers buy somewhere along that arc and grow toward the upper end when volume justifies it.
Stage configurations
Stage 1 - Runout table, manual offload
Stage 2 - Powered kicker, lift table, operator stack
Stage 3 - Auto-bundler, strapping, exit conveyor
Custom - Engineered to your bundle weight and footprint